







RRP Box – Retail-Ready Packaging
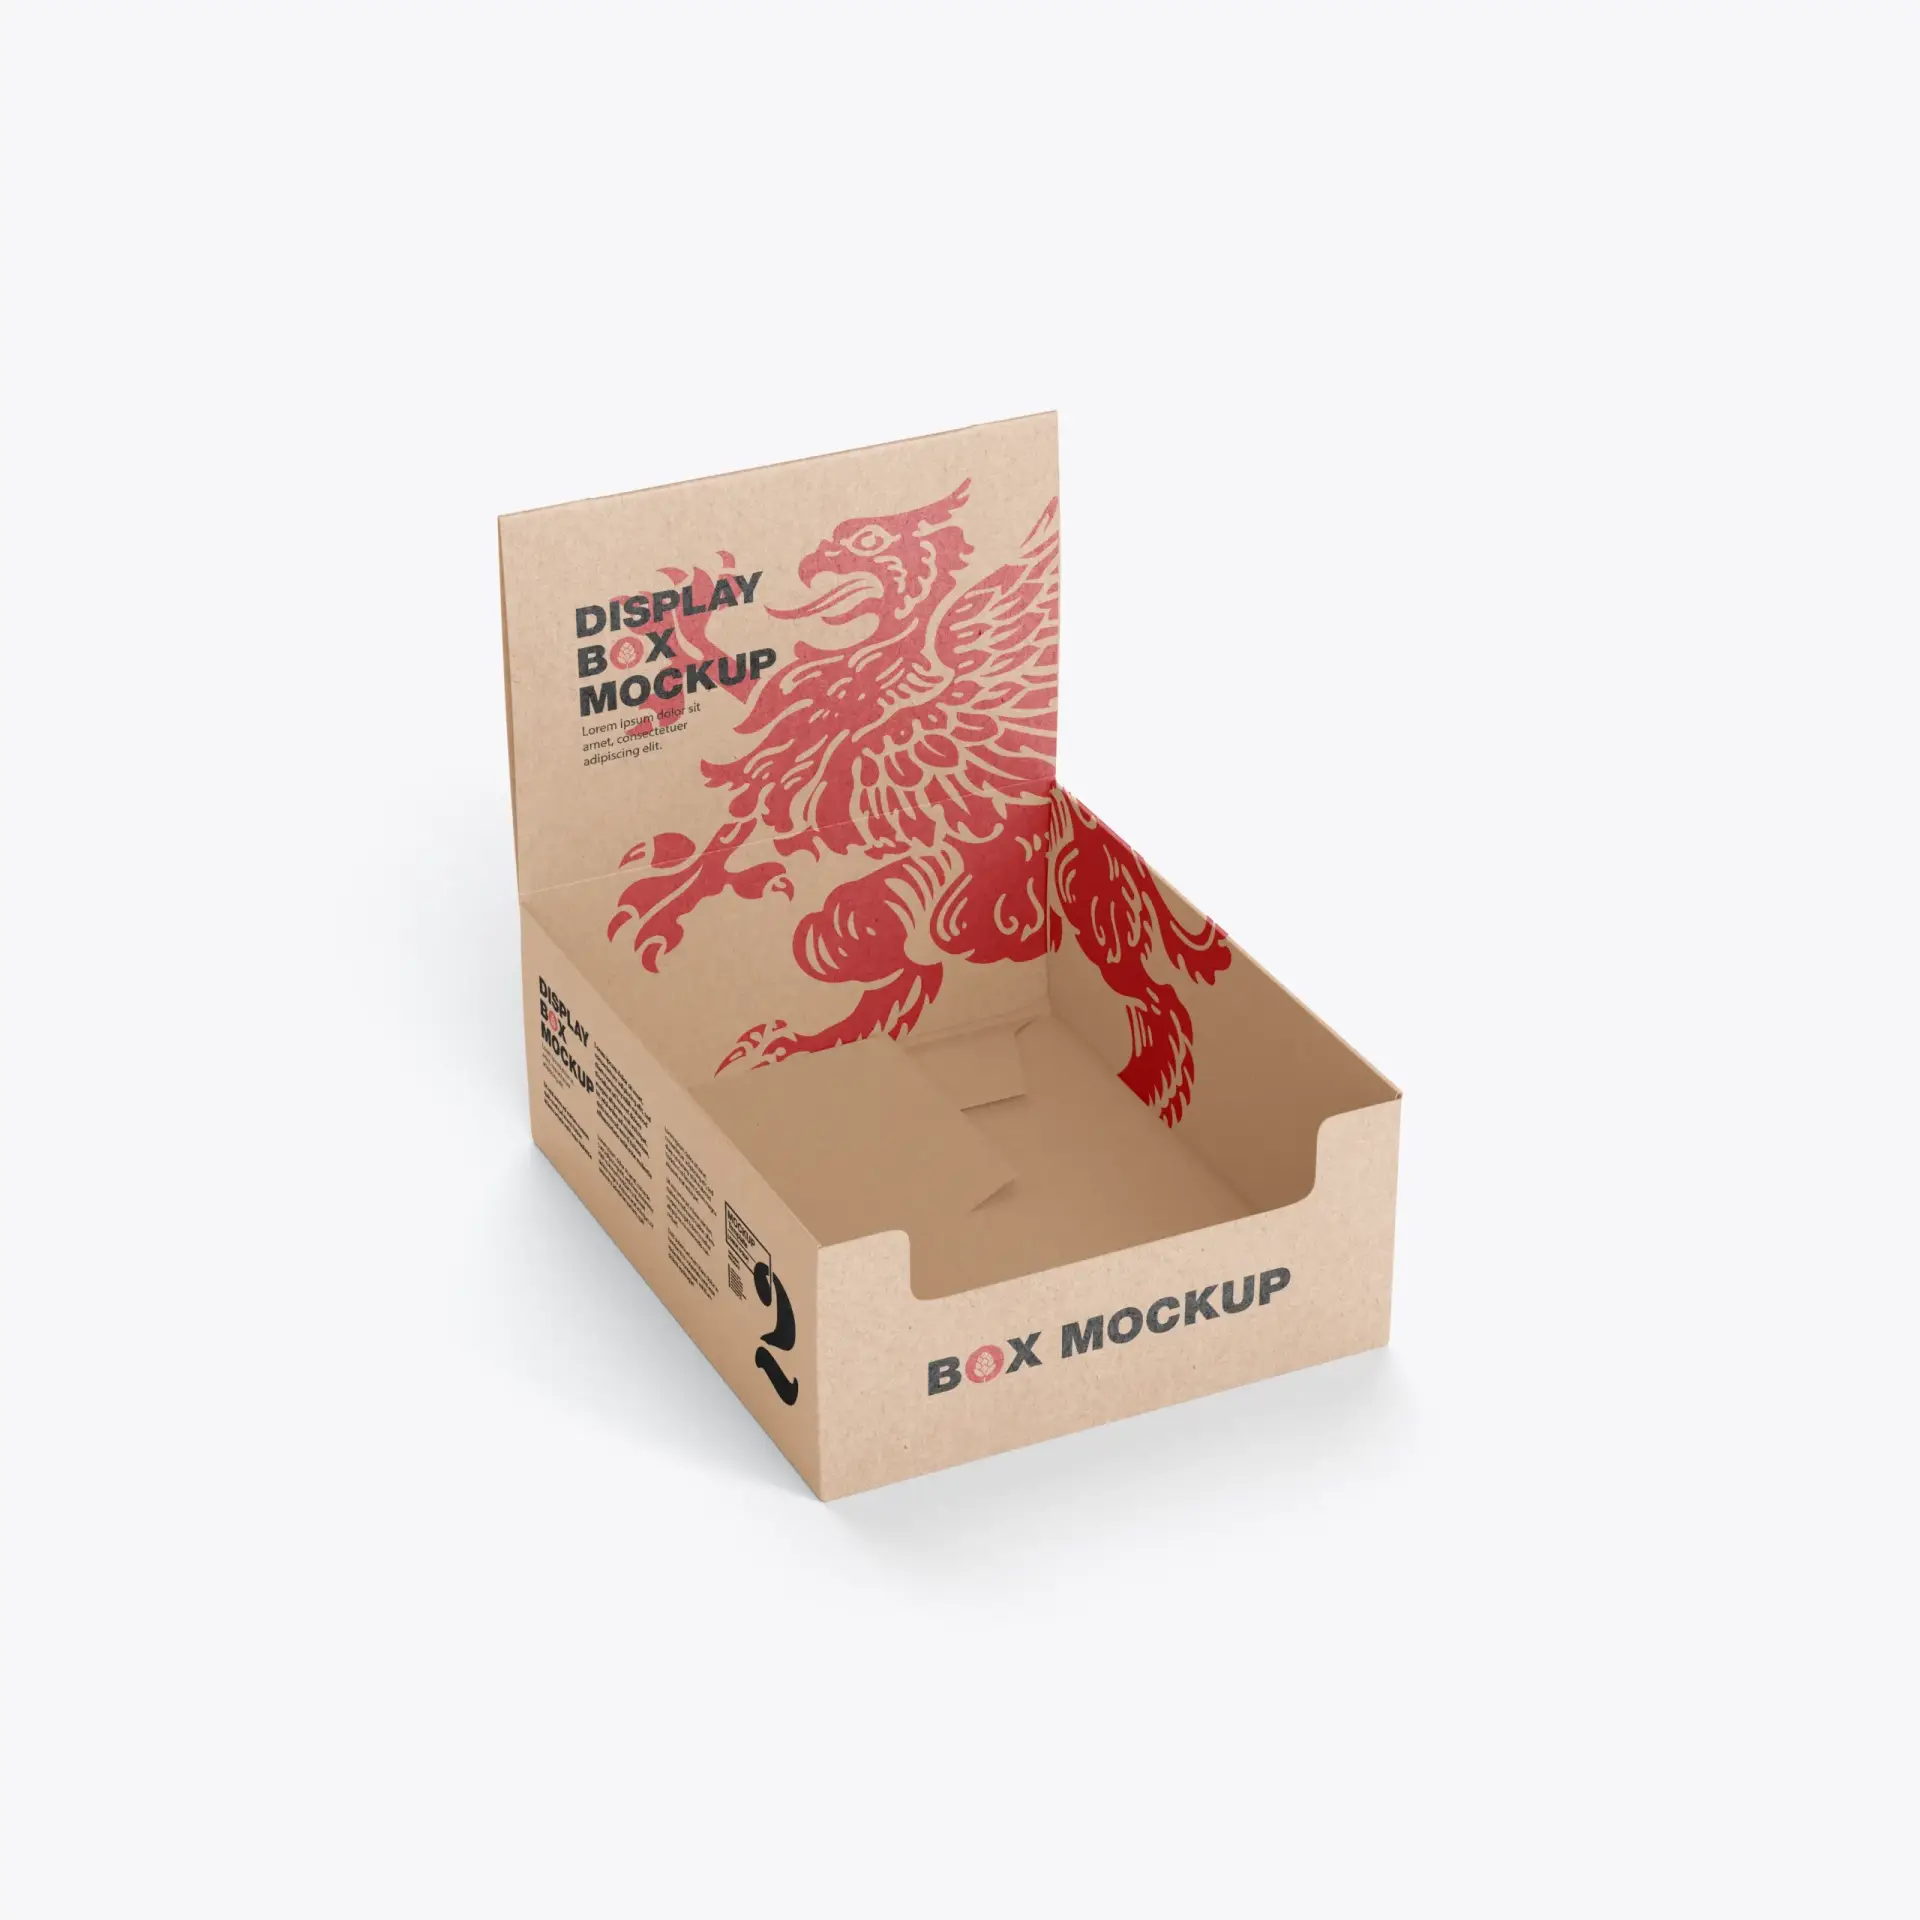
Retail-Ready Packaging (RRP) boxes offer a convenient and impactful way to display products directly on store shelves. Designed for both protection during transport and visual appeal in retail settings, RRP boxes are ideal for consumer goods that need to stand out and be accessed easily.
Suitable for: Variety types of product
Weight: Contact for more information
Size: Contact for more information
Category: Custom Paper Boxes
Tags: RRP, RRP box, Retail-ready packaging, Shelf-ready packaging, Display box, Product display packaging, Display box for retail, Cardboard display box
1. Products That can be Packaged in RRP Boxes
RRP boxes are a versatile packaging option widely used in the snack food, beverage, personal care, electronics, and FMCG sectors. Perfect for multipacks, pouches, bottles, sachets, and cartons, they enhance product visibility while ensuring neat, organized presentation.


2. Functionality of RRP Boxes
RRP boxes are built to serve dual purposes—secure shipping and immediate retail display. Designed with easy-open features and structured layouts, they eliminate the need for additional unpacking or shelf arrangement by store staff.
Key Features:
- Retail-Ready Design: Pre-perforated openings and tear-away tops allow instant shelf display without additional setup.
- Cost-Effective Logistics: Protects products during transport while reducing handling time in stores.
- Shelf Impact: Enhances branding and shopper engagement with eye-level exposure and clean presentation.
- Sustainable Option: Made with recyclable materials, often in line with retailers’ eco standards.
3. Materials and Customization for RRP Boxes
RRP boxes are typically made from corrugated cardboard or rigid paperboard to ensure durability while offering excellent printability for branding. Customization options include:
- High-Quality Offset or Flexo Printing: For vivid branding and messaging.
- Custom Shapes and Sizes: Tailored to fit specific product dimensions.
- Functional Add-ons: Tear strips, handles, or reinforced edges for added usability.
RRP boxes combine efficiency, durability, and marketing value, making them an increasingly preferred packaging choice for modern retail. They streamline the supply chain, boost shelf appeal, and help brands connect with customers directly at the point of sale—all while being environmentally responsible.
Whether you’re launching a new snack line, cosmetics, or daily essentials, RRP boxes offer a clean, professional, and ready-to-display solution that meets the demands of today’s retail environment.

Step 1: Product Preparation
Before packing, all products are sorted by type, size, and quantity to ensure uniformity. Items—such as snack packs, sachets, or small cartons—are inspected for quality and consistency. Proper alignment and orientation are considered to maximize space and ensure a tidy, market-ready display once the box is opened.
Step 2: Selecting the RRP Box
The appropriate RRP box is chosen based on the product dimensions, weight, and retail requirements. Boxes are made from corrugated or rigid cardboard and selected for durability, print finish (e.g., matte, glossy, UV-coated), and perforation features for easy display. Branding elements such as logos, product images, and usage instructions are pre-printed on the box surface.
Step 3: Arranging Products Inside
Products are manually placed into the RRP box following a pre-determined layout for optimal visibility and balance. The placement is designed to minimize movement during transit and ensure the box can be opened directly into a clean, organized shelf display.
Step 4: Perforation and Display Preparation
Perforated lines and tear-away panels are checked to ensure clean removal upon arrival at retail. Some boxes include easy-pull tabs or punch-out windows that reveal product branding and facilitate quick shelf placement without the need for unpacking.
Step 5: Quality Assurance
Each assembled RRP box undergoes a final quality inspection. This includes checks for accurate product count, label alignment, structural integrity, and print quality. Any defects in die-cutting, print smudges, or improper folding are corrected before sealing.
Step 6: Sealing and Stability
Once verified, RRP boxes are closed and sealed using adhesive tape, glue, or interlocking flaps. The design ensures stability during transportation while allowing for easy opening in-store. If required, internal dividers or padding may be added to protect fragile products.
Step 7: Palletizing and Final Touch
Sealed RRP boxes are stacked and palletized for distribution. Care is taken to prevent deformation or crushing. Each pallet is labeled with tracking information and handling instructions. The result: a visually appealing, shelf-ready box that saves time for store staff and provides immediate impact for consumers.
CONTACT US FOR QUOTATION
If you want to request quotation or any assistance, please leave your information here


